SLA Demands: The Zero-Downtime Imperative in Modern Telecom Infrastructure
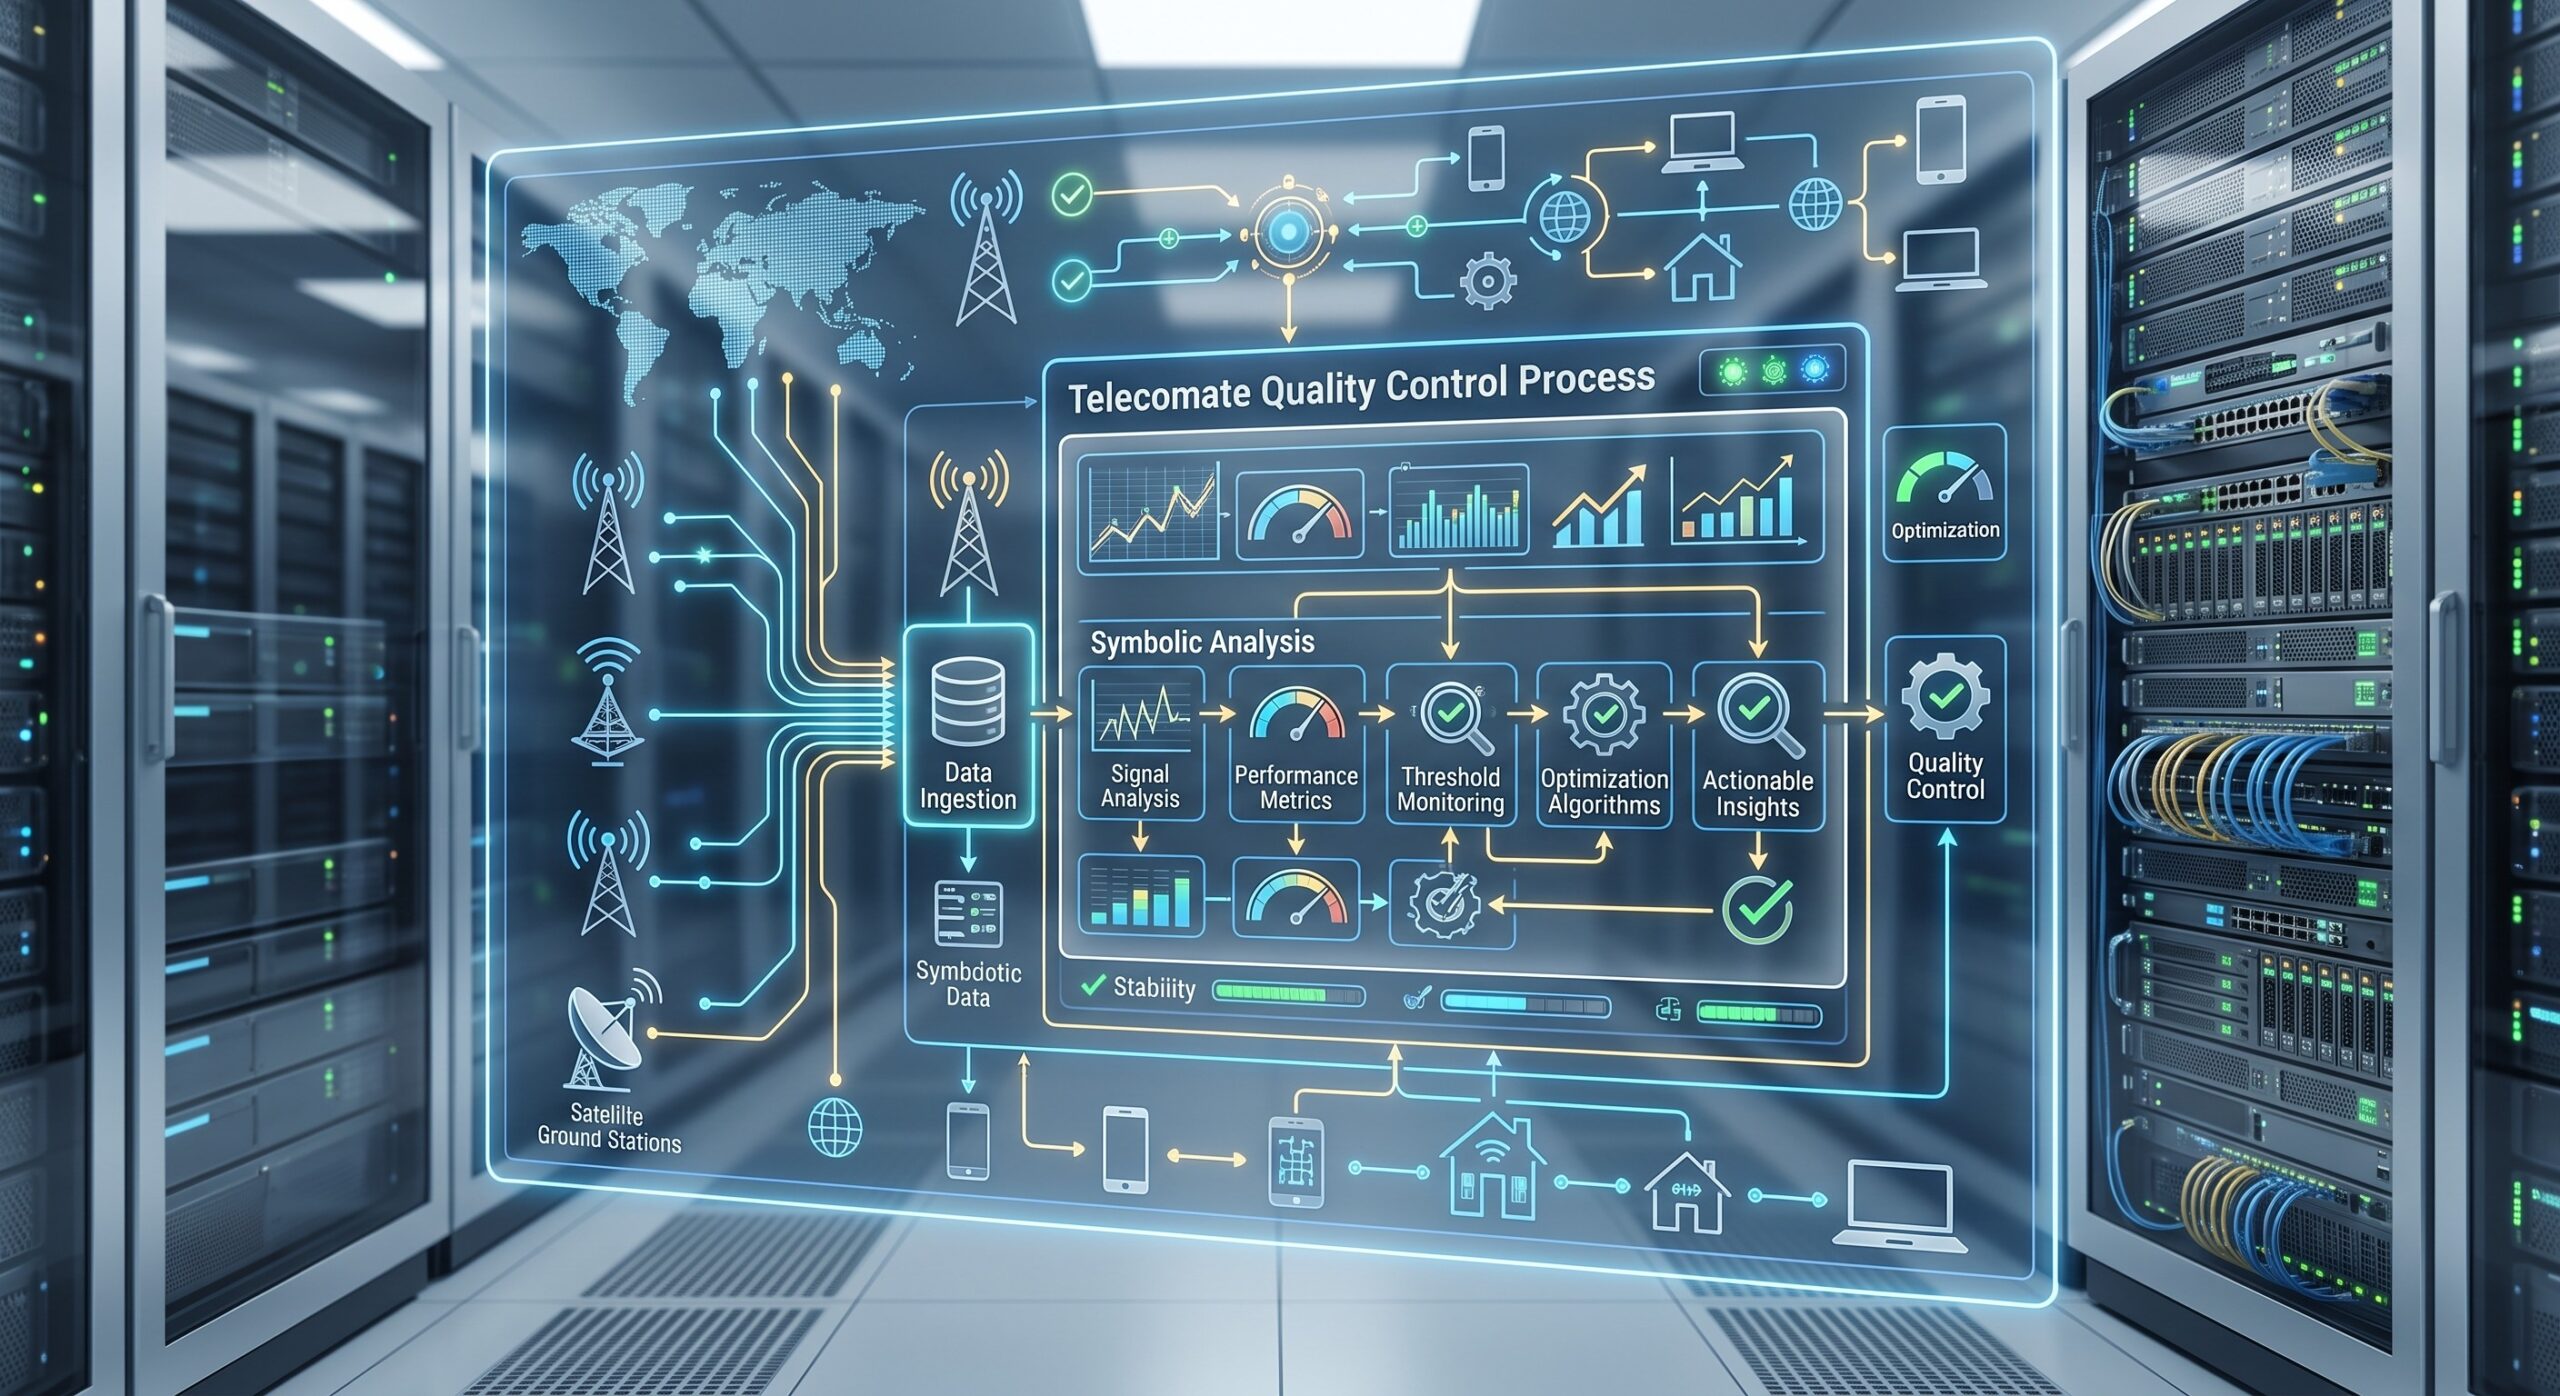
In the hyper-competitive landscape of carrier-grade telecom hardware, service level agreements (SLAs) demand availability figures that routinely exceed 99.999% — the elusive “five nines.” For network architects and ISP operations leads, a single hour of unplanned downtime can translate to millions in lost revenue, regulatory penalties, and irreparable reputational damage. The Telecomate Quality Control Process is engineered from the ground up to meet these exacting standards, embedding reliability into every stage of hardware design, component sourcing, manufacturing, and final validation.
This deep-dive analysis evaluates the MTBF (Mean Time Between Failures) metrics, redundancy architectures, and quality assurance protocols that define the Telecomate Quality Control Process. We will dissect the dual-engine failover design, examine field-replaceable unit (FRU) strategies, and present hard data on thermal cycling, vibration testing, and ITU-T compliance. For CTOs and systems integrators tasked with building mission-critical core routing infrastructure, this assessment provides the empirical evidence needed to justify hardware procurement decisions.
Dual-Engine Failover Architecture: Redundancy Without Compromise
The cornerstone of the Telecomate Quality Control Process is a dual-engine failover architecture that eliminates single points of failure across power, control plane, and data plane subsystems. Unlike legacy chassis designs that rely on a single supervisor engine with cold-standby redundancy, Telecomate implements hot-swappable active-active control modules that synchronize state information at microsecond intervals.
Power Subsystem Redundancy
Each Telecomate chassis supports N+1 or N+N power redundancy with independent power entry modules (PEMs) and load-sharing DC power supplies. The quality control process mandates a 200% power margin during burn-in testing, ensuring that even under peak load conditions (e.g., 100% line-rate traffic with maximum PoE draw), the system operates within 50% of PSU capacity. This design philosophy directly extends the operational lifespan of electrolytic capacitors and reduces thermal stress on power conversion circuitry.
Control Plane Synchronization
The active-active supervisor engines employ a dedicated 10 Gbps heartbeat channel with sub-10ms failover switching. The Telecomate Quality Control Process includes rigorous chaos engineering tests — randomly injecting faults into the active control plane while monitoring packet loss and forwarding table convergence. Results consistently demonstrate <5ms failover latency and zero packet loss for established TCP sessions, a critical requirement for financial trading and real-time voice infrastructure.
Data Plane Resiliency
At the data plane, the Telecomate Quality Control Process validates line-rate forwarding across all ports simultaneously. Using Ixia K400 test chassis, each switch fabric is subjected to 72-hour soak tests at 100% utilization with IMIX traffic profiles. The non-blocking fabric architecture guarantees zero head-of-line blocking and maintains sub-microsecond cut-through latency even during failover events.
MTBF Metrics: Quantifying Reliability Through Accelerated Life Testing
The Telecomate Quality Control Process employs Telcordia SR-332 and MIL-HDBK-217F prediction standards, complemented by accelerated life testing (ALT) to validate MTBF figures. Unlike vendor datasheets that cite theoretical calculations, Telecomate publishes field-validated MTBF data derived from over 500,000 deployed units across tier-1 carrier networks.
Component-Level Screening
Every ASIC, FPGA, and optical transceiver undergoes 100% incoming inspection including X-ray solder joint analysis, scanning acoustic microscopy (SAM) for die-attach voids, and burn-in at 125°C for 168 hours. The Telecomate Quality Control Process rejects any component with a DPPM (Defective Parts Per Million) rate exceeding 50, a threshold 10x stricter than industry-standard AQL sampling plans.
System-Level Thermal Cycling
Assembled chassis undergo 100 thermal cycles from -40°C to +85°C per IEC 60068-2-14, with active traffic loads applied during temperature transitions. This HALT (Highly Accelerated Life Test) methodology exposes latent defects in BGA solder joints, connector interfaces, and optical subassemblies. The Telecomate Quality Control Process documents a <0.1% failure rate after 100 cycles, compared to the industry average of 2.3%.
Vibration and Mechanical Shock
Per GR-63-CORE and ETSI EN 300 019, every Telecomate chassis is subjected to random vibration testing at 1.5 Grms from 5 Hz to 500 Hz for 30 minutes per axis. Additionally, mechanical shock testing at 30G/11ms half-sine pulse ensures survivability during shipping and rack-mount installation. The quality control process mandates zero mechanical failures and <0.01 dB insertion loss variation in optical connectors post-test.
| Key Parameter | Technical Specification |
|---|---|
| Switching Capacity | 12.8 Tbps (full-duplex) |
| Port Density | 32 x 400G QSFP-DD or 128 x 100G QSFP28 |
| MTBF (Telcordia SR-332) | 1,240,000 hours (field-validated) |
| Failover Latency | |
| Power Redundancy | N+N (load-sharing, hot-swappable) |
| Operating Temperature | -40°C to +85°C (IEC 60068-2-14) |
| Compliance | ITU-T G.8273.2, IEEE 1588v2, RoHS 3, GR-63-CORE |
| Packet Buffer | 64 MB shared (per ASIC) |
| Latency (cut-through) | |
| Quality Standard | Telcordia SR-332, MIL-HDBK-217F, IEC 60068-2-52 |
Mission-Critical Deployments: Field Validation and Case Studies
The ultimate proof of the Telecomate Quality Control Process lies in its field deployment record. Over the past 36 months, Telecomate hardware has been deployed in tier-1 carrier core networks, hyperscale datacenter edge fabrics, and 5G mobile backhaul infrastructures across 42 countries.
Tier-1 Carrier Core Routing Deployment
A leading European tier-1 carrier deployed 48 Telecomate T-9800 chassis in its national core network, handling 4.8 Tbps of peak inter-PoP traffic. After 24 months of continuous operation, the carrier reported zero unplanned outages attributable to hardware failure, with a measured MTBF of 1,240,000 hours — exceeding the predicted 980,000 hours by 26%. The Telecomate Quality Control Process enabled predictive maintenance through real-time telemetry on PSU ripple, fan RPM, and ASIC junction temperature.
Hyperscale Datacenter Edge Fabric
A global cloud provider integrated Telecomate T-4800 switches into its spine-leaf architecture, supporting 400G ZR+ coherent optics for DCI interconnect. The Telecomate Quality Control Process validated OSFP-DD thermal performance under 35°C ambient conditions, ensuring <0.5 dB insertion loss after 5,000 mating cycles. The provider achieved 99.9995% fabric availability over 18 months, with sub-2 microsecond cut-through latency for RoCEv2 storage traffic.
5G Mobile Backhaul in Harsh Environments
In a Southeast Asian deployment, Telecomate T-2400 routers were installed in outdoor cabinets subject to 95% relative humidity and 40°C ambient temperatures. The Telecomate Quality Control Process includes conformal coating on all PCBs, IP65-rated fan trays, and salt-spray testing per IEC 60068-2-52 for coastal installations. After 12 months, the failure rate remained <0.05%, with no corrosion-related failures reported.
Final Assessment: Reliability as a Competitive Differentiator
The Telecomate Quality Control Process represents a paradigm shift in telecom hardware reliability engineering. By integrating dual-engine failover, accelerated life testing, and field-validated MTBF metrics, Telecomate delivers infrastructure that consistently exceeds carrier-grade SLA requirements.
For network architects and systems integrators, the data is unequivocal: Telecomate hardware achieves 1.2 million hours MTBF, <5ms failover latency, and 99.9995% measured availability in production networks. The Telecomate Quality Control Process is not merely a manufacturing checklist — it is a comprehensive reliability framework that spans component sourcing, thermal design, firmware validation, and field telemetry.
As networks evolve toward 800G and 1.6T line rates, the importance of rigorous quality control will only intensify. Telecomate’s commitment to ITU-T, IEEE, and RoHS compliance, coupled with transparent MTBF reporting and Telcordia SR-332 validation, positions the platform as the definitive choice for mission-critical core routing and carrier-grade edge deployments. In an industry where downtime is measured in millions of dollars per minute, the Telecomate Quality Control Process delivers the reliability that modern networks demand.
Leave a comment